One of the most common questions we get from distributors and industrial buyers is: should I stock bimetal or carbide band saw blades? The honest answer is: it depends on what your customers are cutting. This guide gives you a clear, practical framework to make the right call.
The Core Difference
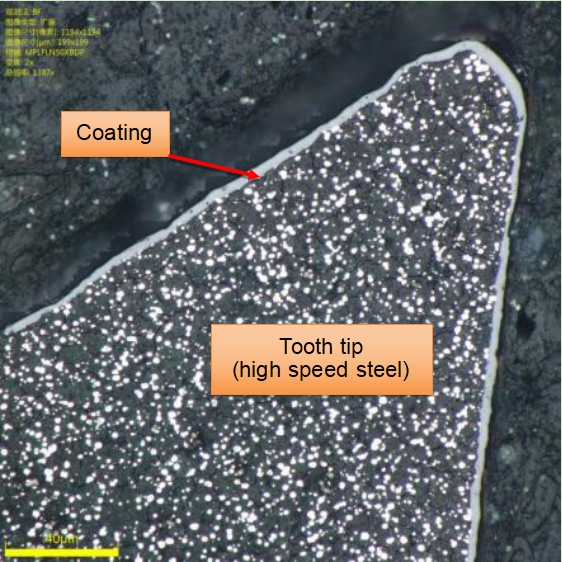
Bimetal band saw blades are made by electron-beam welding high-speed steel (M42 or M51) tooth tips onto a spring-steel backing. The result is a blade that combines flexibility with solid cutting performance across a wide range of materials.
Carbide band saw blades use tungsten carbide tips brazed onto the teeth. Carbide is significantly harder than HSS — roughly 3x harder on the Rockwell scale — which translates to much longer service life when cutting abrasive or very hard materials.
Head-to-Head Comparison
| Factor | Bimetal | Carbide |
|---|---|---|
| Initial cost | Lower | Higher (2–4x bimetal) |
| Service life (mild steel) | Good | Excellent |
| Service life (hardwood/abrasive) | Moderate | Outstanding |
| Cutting speed | Medium–high | High |
| Shock resistance | Excellent | Good (carbide is brittle) |
| Re-sharpening | Possible | Requires diamond wheels |
| Best for | General metalworking, structural steel, pipes | Hardwood, abrasive materials, high-volume production |
When to Choose Bimetal
Bimetal blades are the workhorse of the band saw world. Choose bimetal when:
- Your customers cut carbon steel, alloy steel, or structural profiles
- Cutting conditions include interrupted cuts or vibration — bimetal handles shock far better than carbide
- Your customers run medium-volume operations where blade cost per cut is secondary to upfront price
- You need a universal blade that handles multiple material types without switching
When to Choose Carbide
Carbide blades justify their higher price in specific, high-demand applications. Choose carbide when:
- Cutting hardwoods, teak, bamboo, or engineered wood at volume
- Processing graphite, fiberglass, or other abrasive composites
- Running high-production sawmills where blade changes slow throughput
- Customers need premium surface finish to minimize downstream processing
The Total Cost of Ownership Argument
Many buyers focus on purchase price and overlook the full cost picture. A carbide blade that costs 3x more but lasts 5x longer is actually the cheaper option per meter of material cut. A simple framework:
- Cost per meter cut = (Blade price) ÷ (Total meters cut before replacement)
- Track this metric for both blade types in your customers’ applications
- The blade with the lower cost-per-meter is the right choice — regardless of sticker price
WOKELI Supplies Both
WOKELI manufactures both bimetal and carbide band saw blades at our factories in Sichuan, Jiangsu, and Hubei. Our sales engineers can help you specify the right blade for your customers’ applications based on material, machine speed, and volume.
We supply distributors across Europe and North America with factory-direct pricing, OEM labeling, and flexible MOQ. Request a sample set and see the difference firsthand.